Blog

What Is a Tube Bender and What Types Are Available?

A tube bender is a machine or hand tool that shapes metal tubing into accurate curves without cutting it. It supports work in automotive frames, plumbing systems, furniture, aerospace structures, and industrial equipment. Instead of forcing a straight tube around an improvised object, fabricators use controlled pressure and carefully selected tooling. The result can be cleaner, stronger, and more consistent.

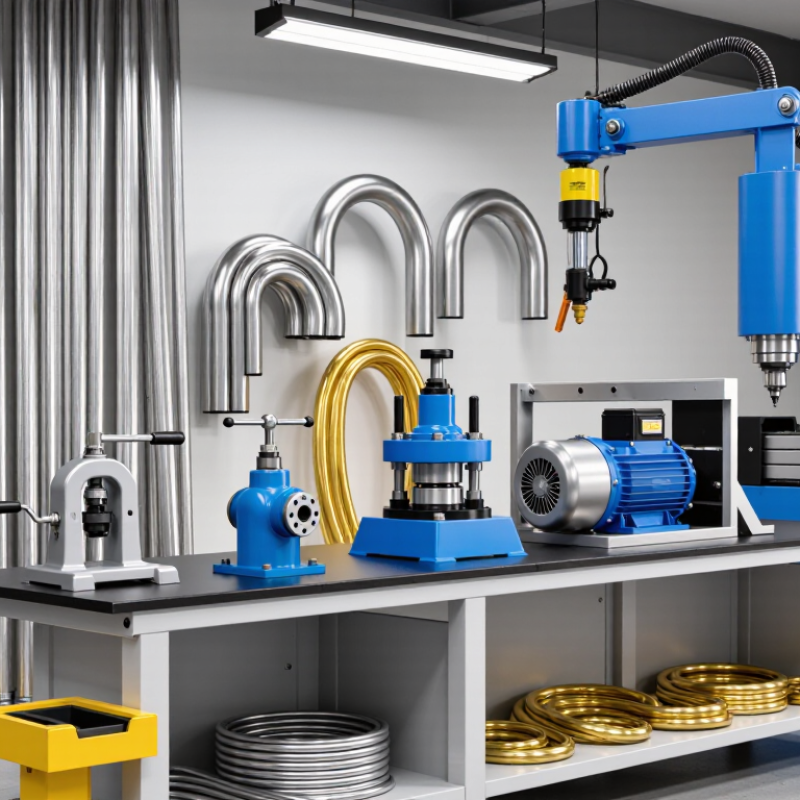
Tube Benders range from compact manual tools to advanced CNC machines. Manual benders suit thin-wall tubing, repair work, and occasional fabrication. Hydraulic models provide greater force for larger diameters and thicker materials. Electric and CNC benders improve repeatability, especially when a project requires many identical parts. Different bending methods also matter. Rotary draw bending creates precise angles, while roll bending produces broad, gradual curves. Compression bending can be useful for simpler shapes, although it may leave more visible deformation.

Choosing the right type depends on tube material, diameter, wall thickness, bend radius, and production volume. It also depends on the operator’s experience. A powerful machine cannot correct poor measurements or unsuitable dies. Even experienced fabricators sometimes underestimate springback, the slight return toward the original shape after bending. That detail can shift an angle by several degrees. Careful testing helps, but no single machine fits every workshop. This guide examines the main tube bender types, their practical strengths, their limitations, and the situations where each design makes sense. Some choices remain difficult. That is normal.

What Is a Tube Bender and What Types Are Available?

What Is a Tube Bender and How Does It Work?

A tube bender is a machine that forms straight tubing into controlled curves without cutting it. It works by applying force around a die. The tube follows the die’s radius, while a clamp holds it firmly. A pressure die supports the outside wall and limits flattening. For tighter bends, a mandrel enters the tube. It supports the inner wall and reduces wrinkles.

The common rotary-draw bender rotates the tube around a fixed die. It produces accurate bends for frames, exhaust systems, handrails, and fluid lines. Roll benders use several rollers and create broad, gradual curves. Compression benders press the tube against a stationary form. They are simpler, but they may distort thin tubing. Electric systems offer repeatable movement, while hydraulic machines handle larger diameters and heavier wall thicknesses.

Scale matters here. The World Steel Association reported approximately 1.88 billion tonnes of crude steel production in 2024, showing the enormous material base behind fabricated tube products. Yet steel volume does not guarantee good bends. Operators still need the correct bend radius, tooling clearance, wall thickness, and springback allowance. A 2024 manufacturing outlook from the International Federation of Robotics also reported continued automation growth across industrial production. That trend supports programmable bending cells, although programming errors remain possible. I have found that a slower test bend often prevents expensive scrap. The first setting is rarely perfect.

Key Components and Bending Principles of Tube Benders

What Is a Tube Bender and What Types Are Available?
Key Components and Bending Principles of Tube Benders

A tube bender shapes metal tubing without cutting or welding the bend. Its core assembly usually includes a bend die, clamp die, pressure die, and carriage. The bend die controls the centerline radius. The clamp die holds the tube firmly. The pressure die supports the outside wall during rotation. For thin-wall tubing, a mandrel can support the inside surface, while a wiper die reduces wrinkling near the tangent point. Small details matter.

Rotary draw bending offers accurate, repeatable angles for frames, fluid lines, and heat-management systems. Roll bending creates larger radii with gradual forming. Compression bending uses a fixed radius and suits simpler geometries. The International Energy Agency’s Global EV Outlook 2024 reported nearly 14 million electric cars sold in 2023. This growth increases demand for compact cooling, structural, and hydraulic tube assemblies. Bending accuracy directly affects packaging space and leak prevention.

The process depends on bend allowance, springback, wall thinning, and ovality. Engineers calculate the neutral axis, then validate the result with material-specific testing. A harder alloy may spring back more than expected. Not quite predictable. A mandrel may prevent collapse, but excessive pressure can mark the tube or distort its diameter. In production, operators should measure angle, radius, and wall thickness after trial bends. A clean equation helps, yet it never replaces inspection. That is where practical experience remains essential.

Manual, Electric, Hydraulic, and CNC Tube Bender Types

A tube bender reshapes metal tubing without cutting it. It supports frames, handrails, vehicle exhausts, and fluid lines. The correct machine depends on tube diameter, wall thickness, bend radius, and production volume. Small shops notice this.

Manual tube benders suit repairs, prototypes, and low-volume work. Operators apply force through a lever, so setup remains simple and affordable.

Electric models add powered rotation and repeatable motion. They reduce physical effort and improve consistency for medium production.

Hydraulic benders deliver higher force for large or thick-wall tubes. However, they may need more floor space and careful die alignment.

CNC tube benders control feeding, rotation, and bending through programmed axes. They offer accurate multi-plane shapes and faster repeat production, but programming skill is essential.

The International Energy Agency reports continued growth in electric-vehicle manufacturing, increasing demand for lightweight tubing and precise formed parts. Grand View Research also identifies rising automation as a major trend in metal-forming equipment. These reports do not make CNC the best choice for every workshop. That assumption needs questioning. A manual machine can outperform an automated system when batches are small.

Tips: Measure the actual outside diameter and wall thickness before selecting tooling. Test one sample tube first. Inspect wrinkles, flattening, springback, and cracking. Keep a bend log with die size, angle correction, and material grade. Even experienced operators sometimes trust machine settings too quickly. Safety glasses, secure clamping, and clear hand positions remain necessary.

How to Choose a Tube Bender for Different Applications

A tube bender shapes metal tubing without crushing its walls. Common types include manual, hydraulic, electric, and CNC models. Manual benders suit small repairs and occasional projects. Hydraulic tools provide greater force for thicker steel or stainless steel tubes. Electric and CNC benders improve speed, repeatability, and production accuracy.

Choosing the right tube bender depends on tube diameter, wall thickness, material, bend angle, and required quantity. Check the machine’s capacity before judging its appearance. A tool designed for thin aluminum may fail on heavy steel tubing. For tight bends, confirm the minimum bend radius and use the correct die. Poor die matching can leave wrinkles, flat spots, or visible marks. In practical workshop settings, testing one sample tube first can prevent expensive material waste. It is easy to focus on power, but control often matters more.

Tips: Measure the tube carefully. Mark the bend location clearly. Support long sections during operation. Lubricate when the tool instructions require it. Inspect the first finished bend with a template or angle gauge. Remember that a stronger machine is not always the better choice. Manual tools can offer better control for delicate work, while automated equipment may need more setup than expected. Reconsider the choice if operators lack training or the workspace cannot support safe handling.

Safe Operation and Maintenance of Tube Bending Equipment

What Is a Tube Bender and What Types Are Available?

Tube bending equipment ranges from manual lever tools to hydraulic, rotary-draw, roll, and CNC systems. Each type needs a different safety routine. Before bending, verify the tube’s material, diameter, wall thickness, and required bend radius. Never rely on appearance alone.

Inspect the frame, clamps, dies, guards, hoses, and electrical controls before each shift. Keep hands clear of pinch points. Stop immediately. Secure the tube firmly, then confirm that the die and clamp match its size.

Wear eye protection, safety footwear, and close-fitting work clothes. Loose sleeves can catch unexpectedly. Keep the floor dry and remove cutoffs from the work area.

Use the machine’s specified lubricant and avoid excessive application near electrical parts. Check hydraulic lines for leaks, unusual swelling, or damaged fittings. Isolate power before cleaning, adjusting, or replacing tooling. A test bend on scrap material can reveal incorrect settings without wasting production tubing.

Record inspection results, lubrication dates, pressure readings, and tooling changes. Small errors matter. Even trained operators may skip a check during a busy shift, so a visible checklist helps expose that weakness. Recalibrate the equipment when bends drift, springback changes, or measurements become inconsistent. Maintenance is not only repair work; it is careful observation repeated before problems become injuries or rejected parts.
Article Source:

Go to Top